What Is CNC Turning? Process, Applications, and Benefits
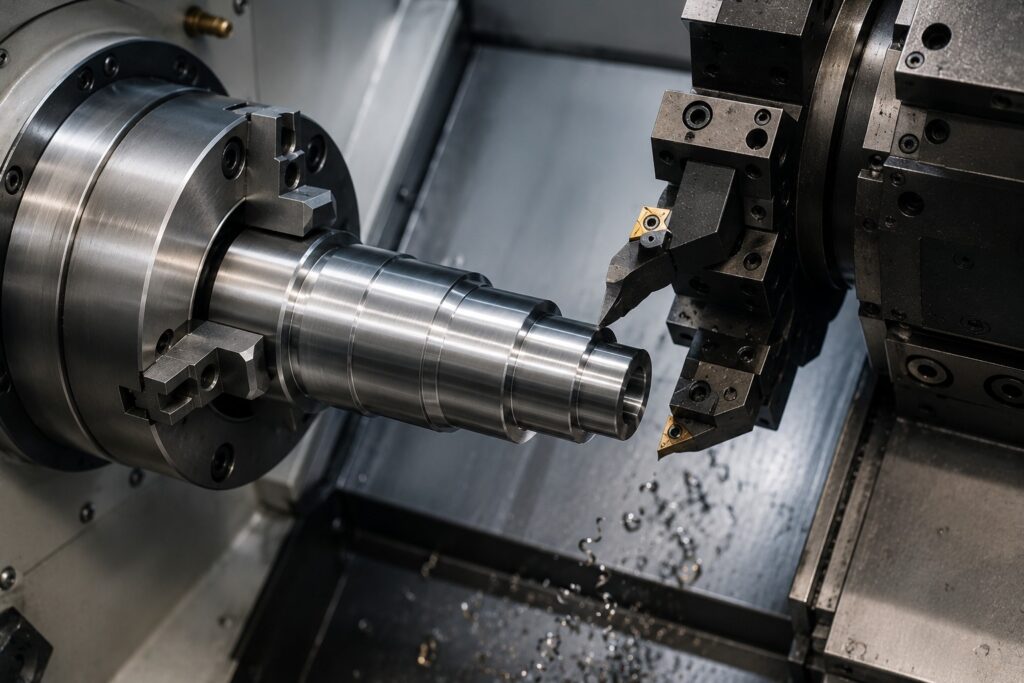
Introduction CNC turning is a widely used manufacturing process for producing cylindrical and rotational components with consistent dimensions and repeatable quality. It uses computer-controlled equipment to rotate a workpiece while cutting tools remove material according to programmed instructions. From shafts and pins to bushings, sleeves, rollers, and threaded components, CNC turning can manufacture a wide range of custom parts. Therefore, it is an important process for industries that require accurate and repeatable rotational components. At Polymach365, CNC manufacturing solutions support custom components, prototypes, low-volume production, and production parts using digital manufacturing workflows. What Is CNC Turning? CNC turning is a subtractive manufacturing process in which a workpiece rotates while a cutting tool removes material to create the required shape. CNC stands for Computer Numerical Control. Instead of manually controlling the cutting operation, the machine follows programmed instructions generated from the component’s digital design. CNC turning is particularly suitable for components with rotational geometry, including: Shafts Pins Bushings Sleeves Rollers Spacers Couplings Threaded components Cylindrical housings As a result, CNC turning can produce both simple and complex rotational parts with repeatable dimensions. How Does CNC Turning Work? The CNC turning process typically follows these steps: CAD Design → CAM Programming → Material Preparation → Machine Setup → CNC Turning → Inspection → Finishing → Delivery 1. CAD Design The process begins with a digital CAD model or engineering drawing. The design defines the required dimensions, diameters, lengths, threads, grooves, holes, and other features. 2. CAM Programming CAM software converts the design into machine-readable toolpaths. The program determines: Tool movements Cutting speeds Feed rates Cutting depths Machining sequence 3. Workpiece Setup The raw material is secured in the machine using a chuck or another suitable workholding method. The correct cutting tools are then installed. 4. Material Removal The workpiece rotates while the cutting tool moves against it. Material is gradually removed until the required geometry is achieved. Different tools can be used for operations such as roughing, finishing, threading, grooving, and drilling. 5. Inspection The finished component is inspected to verify dimensions and other specified requirements. Therefore, inspection helps ensure the component matches the approved design. What Parts Can Be Made Using CNC Turning? CNC turning is ideal for components with rotational or cylindrical features. Common CNC turned parts include: Shafts Used in machinery, motors, automation equipment, and mechanical assemblies. Pins Used for alignment, fastening, and mechanical connections. Bushings Used to reduce friction and support moving components. Spacers Used to maintain specific distances between components. Sleeves Used in mechanical and industrial assemblies. Rollers Used in machinery, material-handling systems, and automation. Threaded Components CNC turning can produce external and internal threaded features when appropriate tooling and processes are used. Therefore, CNC turning can support many mechanical and industrial applications. CNC Turning Process Operations Different operations can be performed on a CNC turning machine depending on the part design. Facing Facing creates a flat surface on the end of the workpiece. Turning Turning reduces the diameter of the workpiece to the required dimension. Boring Boring enlarges or finishes an existing internal hole. Drilling Drilling creates holes in the workpiece. Threading Threading produces internal or external threads. Grooving Grooving creates narrow recesses or channels. Parting Parting separates the finished component from the remaining material. Therefore, multiple turning operations can be combined to manufacture a complete component. CNC Turning Machine Types Different CNC turning machines are available for different manufacturing requirements. CNC Lathe A CNC lathe rotates the workpiece while cutting tools perform the required machining operations. It is suitable for many standard cylindrical components. CNC Turning Center A turning center can combine turning with additional operations such as drilling and other machining processes. As a result, it can reduce the need for transferring components between different machines. Multi-Axis Turning More advanced CNC turning equipment can provide additional machine movement and tooling capabilities for more complex components. Therefore, the appropriate machine configuration depends on the geometry, quantity, and manufacturing requirements of the part. Materials Used for CNC Turning CNC turning can be performed on many metals and engineering plastics. Common materials include: Aluminum Stainless steel Carbon steel Alloy steel Tool steel Brass Copper Titanium Nylon Delrin PEEK Other engineering plastics Aluminum Aluminum is widely used because it is lightweight and generally easy to machine. Stainless Steel Stainless steel is suitable when strength and corrosion resistance are important. Brass Brass offers good machinability and can be used for fittings, bushings, connectors, and other components. Titanium Titanium offers a high strength-to-weight ratio but requires careful machining conditions. Therefore, material selection should consider both the required part performance and manufacturing requirements. Benefits of CNC Turning High Repeatability Computer-controlled machining allows the same programmed operations to be repeated across multiple components. Therefore, CNC turning is suitable for batch and production manufacturing. Consistent Dimensions Controlled machining parameters can help maintain consistent diameters, lengths, and other critical features. Complex Rotational Components CNC turning can produce components containing multiple diameters, grooves, threads, tapers, and other features. Reduced Manual Intervention Once the machine is properly programmed and set up, many machining operations can be performed automatically. Suitable for Prototypes CNC turning can produce functional prototypes directly from digital designs. Suitable for Production The process can also support repeated manufacturing of custom components. As a result, CNC turning can be used throughout different stages of product development. CNC Turning for Prototype Manufacturing Product development often requires functional prototypes before production begins. CNC turning allows engineers to create prototypes that closely represent the intended production component. A typical workflow is: CAD Design → Prototype Machining → Testing → Design Improvements → Production This allows teams to evaluate: Fit Dimensions Assembly Function Mechanical performance Therefore, CNC turning can help identify design issues before production quantities increase. CNC Turning for Low-Volume Production Many businesses require smaller quantities rather than thousands of components. CNC turning can be suitable for: One-off parts Small batches Low-volume production Replacement components Engineering validation Specialized components Because CNC turning does not require dedicated injection-molding tooling for each design, it can provide flexibility when
CNC Milling vs CNC Lathe: Understanding the Right Machine for Your Part
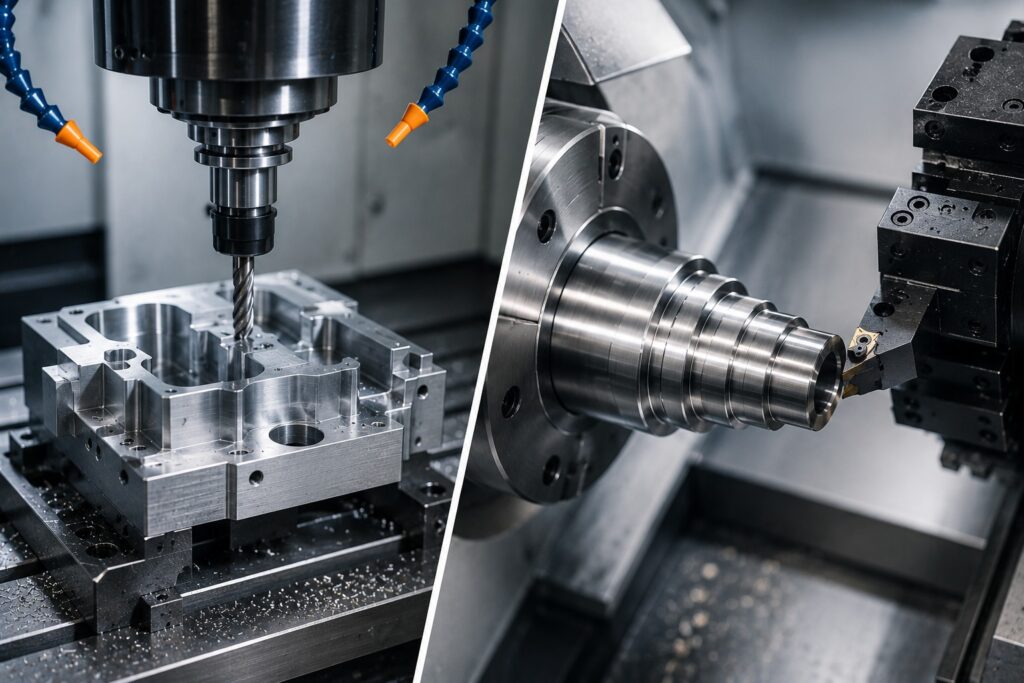
Introduction Choosing between CNC milling and CNC lathe machining is an important decision when manufacturing custom components. Although both are computer-controlled machining processes, they use different cutting methods and are designed for different types of part geometries. CNC milling is generally suited to parts with flat surfaces, pockets, slots, holes, contours, and complex features, while CNC lathe machining is primarily used for round and rotational components such as shafts, pins, bushings, sleeves, and rollers. Understanding the difference between CNC milling and CNC turning can help engineers and manufacturers select the right process based on the part design, material, tolerances, quantity, and production requirements. At Polymach365, digital manufacturing solutions support CNC milling, CNC turning, multi-axis machining, prototypes, custom components, and production requirements. What Is CNC Milling? CNC milling is a subtractive manufacturing process that uses rotating cutting tools to remove material from a workpiece. The cutting tool moves along programmed axes to create the required geometry. Depending on the machine configuration, CNC milling can produce features on multiple sides of a component. Common CNC milling features include: Pockets Slots Holes Flat surfaces Contours Threads Angled surfaces Complex 3D profiles Therefore, CNC milling is particularly useful for components with non-rotational or complex geometries. What Is CNC Lathe Machining? CNC lathe machining, commonly called CNC turning, rotates the workpiece while a cutting tool removes material. The rotating workpiece allows the cutting tool to create cylindrical and rotational features. Typical CNC lathe components include: Shafts Pins Bushings Sleeves Rollers Spacers Couplings Cylindrical housings Threaded components As a result, CNC lathe machining is often the preferred process for round or rotational parts. CNC Milling vs CNC Lathe: Key Difference The main difference is how the workpiece and cutting tool move. CNC Milling The cutting tool rotates and moves around a generally stationary workpiece. CNC Lathe The workpiece rotates while the cutting tool moves against it. This fundamental difference determines the types of geometries each machine can efficiently manufacture. CNC Milling vs CNC Lathe Comparison Feature CNC Milling CNC Lathe Primary movement Rotating cutting tool Rotating workpiece Best for Complex and prismatic parts Cylindrical and rotational parts Common features Pockets, slots, holes, contours Diameters, threads, grooves, tapers Typical parts Brackets, housings, plates Shafts, pins, bushings Multi-sided machining Highly suitable More limited depending on machine Complex 3D geometry Excellent with multi-axis machines Better suited to rotational geometry Common operations Milling, drilling, pocketing Turning, facing, boring, threading Typical workpiece shape Blocks, plates, irregular forms Round bars and cylindrical stock When Should You Choose CNC Milling? CNC milling is generally the better choice when your part contains multiple non-cylindrical features. It can be particularly suitable for: Complex Shapes Components with irregular profiles and 3D contours can often be efficiently produced using CNC milling. Pockets and Slots If the design contains multiple pockets, slots, or recessed features, milling is typically appropriate. Flat Surfaces Mounting plates, brackets, housings, and similar components often require several machined flat surfaces. Multiple Holes CNC milling can efficiently create holes at different positions and orientations. Multi-Sided Parts 4-axis and 5-axis machining can provide access to multiple surfaces without requiring as many separate setups. Therefore, CNC milling is a versatile choice for many custom components. When Should You Choose CNC Lathe Machining? CNC lathe machining is generally preferred when the primary geometry is rotational. It is commonly used for: Shafts Long cylindrical components used in machinery, motors, automation, and mechanical assemblies. Bushings Components designed to support movement and reduce friction. Pins Used for alignment, fastening, and mechanical connections. Rollers Used in machinery, automation, and material-handling equipment. Sleeves and Spacers Cylindrical components used in mechanical assemblies. Threaded Components CNC turning can produce external and internal threads using appropriate tooling and machining processes. Therefore, if the majority of your component’s geometry revolves around a central axis, CNC lathe machining may be the more efficient option. CNC Milling Operations CNC milling machines can perform several different operations depending on the part design. Face Milling Creates flat surfaces on the workpiece. Pocket Milling Removes material from enclosed areas to create pockets. Slot Milling Creates channels and slots. Drilling Produces holes in specified locations. Contour Milling Machines external profiles and complex boundaries. Thread Milling Creates threaded features using specialized cutting tools. As a result, multiple operations can often be combined within a single CNC milling setup. CNC Lathe Operations CNC lathes can also perform several operations. Facing Creates a flat end surface. Turning Reduces the diameter of the workpiece. Boring Machines or enlarges internal holes. Drilling Creates axial holes. Threading Produces internal or external threads. Grooving Creates narrow channels or recesses. Parting Separates the finished component from the remaining stock. Therefore, CNC turning can manufacture a complete rotational component through a sequence of machining operations. What About Complex Parts? Some components cannot be classified as purely milling or turning parts. For example, a component may have: A cylindrical body Multiple holes Flat surfaces Slots Threads Complex side features In such cases, a combination of CNC turning and CNC milling may be appropriate. The primary cylindrical geometry can be produced through turning, followed by milling operations for additional features. Therefore, selecting a machining process should be based on the complete part geometry rather than just one feature. 3-Axis, 4-Axis, and 5-Axis CNC Milling CNC milling capabilities vary depending on machine configuration. 3-Axis CNC Milling Suitable for many standard components containing holes, pockets, slots, and flat surfaces. 4-Axis CNC Milling Adds rotational movement, allowing additional surfaces to be machined without completely repositioning the workpiece. 5-Axis CNC Milling Provides greater flexibility for complex geometries, angled surfaces, deep cavities, and multi-sided features. Therefore, more advanced machining capabilities can be useful when a component has difficult-to-access features. CNC Milling vs CNC Lathe for Prototypes Both processes can be useful for prototype manufacturing. Choose CNC Milling When: The prototype has complex geometry. The design contains multiple pockets or slots. Several flat surfaces are required. The part has multiple non-cylindrical features. Choose CNC Lathe When: The prototype is primarily cylindrical. The component contains multiple diameters. Threads or grooves
How CNC Machining Helps Manufacturers Create Repeatable Custom Parts
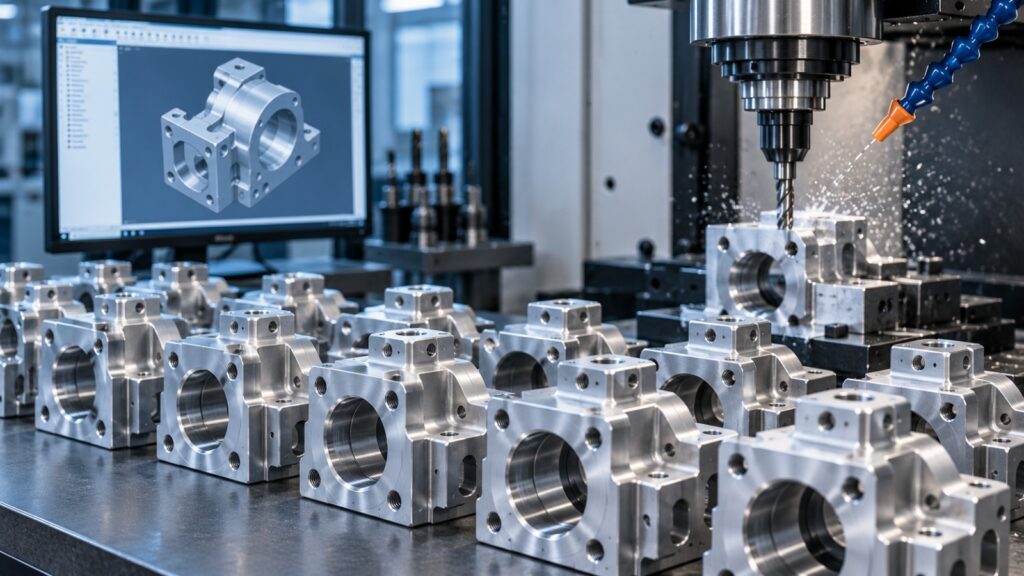
Improving Part Consistency, Accuracy, and Production Efficiency with CNC Manufacturing Manufacturers often need to produce the same custom component multiple times while maintaining consistent dimensions, fit, and performance. This can be challenging when parts require complex geometries, tight tolerances, or multiple machining operations. CNC machining helps manufacturers create repeatable custom parts by using programmed machining instructions, controlled cutting parameters, standardized setups, and quality inspection. Once a machining process has been properly developed and validated, the same digital instructions can be used to reproduce the component with consistent results. For this reason, CNC machining is widely used for custom components, prototypes, replacement parts, low-volume batches, and production manufacturing. What Does Repeatability Mean in CNC Machining? Repeatability refers to the ability to manufacture multiple components that remain consistent with one another and meet the specified engineering requirements. For example, if a manufacturer orders 100 custom brackets, each bracket may need to maintain the same: Overall dimensions Hole locations Hole diameters Thickness Surface finish Threads Critical tolerances Assembly fit Therefore, repeatability is particularly important when components need to work together within an assembly. CNC machining supports this consistency by controlling machining operations through programmed instructions rather than relying entirely on manual cutting and positioning. How CNC Machining Creates Repeatable Custom Parts Several factors work together to make CNC machining suitable for repeatable manufacturing. 1. Digital CAD-Based Manufacturing CNC production generally starts with a digital CAD model or engineering drawing. The design provides the geometry and dimensional requirements that guide the manufacturing process. The digital nature of CNC manufacturing makes it easier to maintain the same design information across repeated production runs. Polymach365’s manufacturing workflow, for example, starts with uploading a 3D CAD file, followed by quoting and production. Supported formats include STEP, STL, IGES, SLDPRT, and ZIP. As a result, manufacturers can establish a consistent digital foundation for producing custom components. 2. Consistent CNC Programs Once the machining strategy has been established, CNC equipment follows programmed toolpaths to perform cutting operations. The program can control: Tool movements Cutting paths Spindle speeds Feed rates Machining sequences Tool changes Workpiece coordinates Consequently, repeated components can be manufactured using the same validated machining strategy. This is one of the major differences between CNC machining and processes that depend heavily on manual operation. 3. Controlled Machining Setups Workholding and positioning have a significant effect on repeatability. If a component is repositioned differently for each operation, small variations can affect the final dimensions. Therefore, establishing a reliable workflow and setup strategy is important for repeated manufacturing. Reducing unnecessary setups can also improve consistency because every additional repositioning can introduce positioning variation. For suitable complex components, multi-axis machining may reduce the number of repositioning operations required. 4. Tool Management and Tool Wear Control Cutting tools gradually wear during machining. As a tool becomes worn, it can affect: Dimensional accuracy Surface finish Cutting performance Feature geometry Production consistency Therefore, monitoring tool condition is particularly important during repeated production. Manufacturers can use appropriate tool selection, tool-life management, offsets, and inspection procedures to identify changes before they significantly affect component quality. 5. Machine Calibration CNC machine condition also affects repeatability. Machine components, spindle systems, guideways, ball screws, and other mechanical elements can influence positioning performance over time. Calibration and verification help manufacturers maintain accurate machine movement and identify potential issues. Important areas include: Axis positioning Machine geometry Spindle alignment Tool offsets Positioning repeatability Therefore, maintaining the machine is an essential part of producing consistent components. 6. Consistent Material Selection Material properties can also influence manufacturing consistency. Different materials behave differently during cutting. Factors such as hardness, thermal expansion, machinability, and material stability can affect the machining process. Common CNC materials include: Aluminum Stainless steel Carbon steel Brass Copper Titanium ABS Nylon Delrin PEEK Selecting a suitable material and maintaining consistent material specifications can help reduce variation between production batches. 7. Design for Manufacture A component’s design can have a greater impact on repeatable production. Features such as extremely thin walls, deep cavities, narrow slots, small internal radii, and difficult-to-access surfaces may require specialized tooling or additional setups. Therefore, Design for Manufacture (DFM) should be considered before production begins. A CNC-friendly design can help improve: Dimensional consistency Tool accessibility Surface finish Assembly fit Machining efficiency Repeatability DFM can also help identify potential manufacturing problems before they become production issues. 8. Quality Inspection Repeatability cannot be established simply by running the same CNC program repeatedly. Manufacturers also need to verify the results. Quality inspection can include checking: Critical dimensions Hole locations Diameters Thickness Flatness Surface finish Threads Geometric features Inspection results can then be used to identify process variation and make necessary adjustments. As a result, quality control becomes an important part of maintaining repeatable custom parts. CNC Milling and Turning for Repeatable Components Different component geometries require different machining processes. CNC Milling CNC milling is commonly used for custom components with: Pockets Slots Holes Flat surfaces Complex profiles Mounting features Contoured surfaces It is suitable for brackets, housings, fixtures, plates, tooling, and many other custom components. CNC Turning CNC turning is generally used for rotational components such as: Shafts Pins Bushings Sleeves Spacers Rollers Threaded components Choosing the appropriate machining process can improve both production efficiency and consistency. The Role of Multi-Axis CNC Machining Complex custom parts may require multiple machining orientations. Using 4-axis or 5-axis machining can provide access to multiple surfaces and complex features without requiring as many separate setups. This can be beneficial because reducing repositioning operations can help minimize potential setup variation. However, not every component requires multi-axis machining. The appropriate process should be selected according to the part geometry, tolerances, material, quantity, and production requirements. Repeatability for Prototypes and Low-Volume Production Repeatability is not limited to large production runs. Manufacturers may need consistent components for: Prototype testing Pilot production Engineering validation Replacement parts Specialized equipment Small production batches Product development CNC machining can support these applications because the same digital design and manufacturing approach can be applied as the project progresses from prototype to production. Polymach365 supports
CNC Machining for Custom Components: From Design to Production
A Practical Guide to Turning CAD Designs into Accurate, Production-Ready Components Modern manufacturers often need components that are designed specifically for a particular machine, product, or application. However, producing a custom component requires more than simply sending a CAD file to a CNC machine. The design, material, tolerances, machining process, quantity, and quality requirements all influence the final result. CNC machining for custom components provides a flexible way to move from an initial digital design to a functional prototype, small batch, or production-ready part. With CNC milling, CNC turning, and multi-axis machining, manufacturers can produce components with complex geometries and precise features. What Is CNC Machining for Custom Components? CNC machining is a subtractive manufacturing process in which computer-controlled cutting tools remove material from a solid workpiece to create the required component geometry. Custom CNC machining is particularly useful when a component must meet specific engineering requirements rather than standard dimensions. Custom components may include: Machine parts Brackets and housings Shafts and bushings Fixtures and tooling Mold components Replacement parts Prototype components Custom industrial components Therefore, CNC machining can support projects ranging from one-off prototypes to repeated production requirements. From CAD Design to CNC Production The CNC manufacturing process starts with a digital design and progresses through several important stages. 1. Create the CAD Design The first step is developing an accurate 3D CAD model or engineering drawing. The design should clearly define important requirements such as: Overall dimensions Critical tolerances Hole sizes Threads Wall thickness Internal radii Surface finish Material requirements A well-prepared design gives the manufacturer the information needed to evaluate how the component should be produced. 2. Review the Design for Manufacture Before machining begins, the component should be reviewed from a manufacturing perspective. This is commonly known as Design for Manufacture (DFM) . A DFM review considers factors such as tool accessibility, tolerances, material, machining orientation, wall thickness, internal corners, and the number of required setups. As a result, potential manufacturing challenges can be identified before production begins. 3. Select the Right Material Material selection directly affects component performance as well as machining requirements. Common CNC materials include: Metals Aluminum Stainless steel Carbon steel Brass Copper Titanium Tool steel Engineering Plastics ABS Nylon Delrin PEEK Polycarbonate PTFE The right material depends on factors such as strength, weight, corrosion resistance, temperature, wear, machinability, and the intended application. Choosing the Right CNC Machining Process Not every custom component requires the same machining process. Therefore, selecting the appropriate process is an important part of production planning. CNC Milling CNC milling is suitable for components with flat surfaces, pockets, slots, holes, contours, and complex profiles. It is commonly used for: Machine housings Plates Braces Fixtures Tooling Complex mechanical components CNC Turning CNC turning is primarily used for rotational components. Typical examples include: Shafts Pins Bushings Sleeves Rollers Spacers Threaded components 3-Axis, 4-Axis, and 5-Axis Machining The number of machining axes can influence how efficiently complex components can be manufactured. For example, 5-axis machining can provide access to multiple surfaces and angled features that may otherwise require several setups. However, the most advanced machining process is not automatically the most economical option. The best approach depends on the component’s geometry, tolerances, material, and production requirements. CNC Machining for Prototypes Custom components often begin as prototypes. Before committing to production, engineers may need to verify: Dimensional accuracy Assembly fit Clearances Function Strength Material selection Surface finish CNC machining can produce functional prototypes directly from CAD designs, allowing engineers to test a physical component and make improvements before production. A typical development cycle is: CAD Design → DFM Review → CNC Prototype → Testing → Design Improvements → Production This approach can reduce the risk of moving an untested design directly into larger production quantities. Moving from Prototype to Production Once a prototype has been tested and approved, the next step may be low-volume or full production. Production machining focuses more heavily on: Repeatability Dimensional consistency Process efficiency Tool life Inspection Cycle time Production scheduling For some projects, low-volume CNC manufacturing provides a useful middle stage between prototyping and larger production. Therefore, a custom component can progress through: Prototype → Design Validation → Low-Volume Production → Process Optimization → Production How to Reduce Custom CNC Component Costs Custom machining does not necessarily have to mean unnecessarily high manufacturing costs. Several design decisions can help control production costs. Use Practical Tolerances Specify tight tolerances only where they are functionally necessary. Extremely tight tolerances can require additional machining and inspection. Simplify Unnecessary Features Avoid features that do not contribute to the component’s function. Simpler geometry can reduce machining time and tooling requirements. Reduce the Number of Setups Where practical, design and manufacture the component to minimize repositioning. Select a Suitable Material Choose a material based on current performance requirements rather than automatically selecting the most expensive option. Avoid Unnecessary Finishing Additional surface treatments and finishing operations should be specified when they provide a functional or required aesthetic benefit. Consequently, thoughtful design decisions can reduce manufacturing costs without compromising essential component performance. Quality Control for Custom CNC Components Quality control should be considered throughout the manufacturing process, not only after machining is complete. Important quality factors include: Dimensional accuracy Tolerance compliance Surface finish Feature location Material specifications Repeatability Assembly fit A typical manufacturing workflow can therefore include: CAD File → Manufacturing Review → CNC Machining → Quality Inspection → Finished Component Providing accurate CAD files together with material, quantity, tolerances, surface finish, and other technical requirements helps establish the appropriate manufacturing approach. Applications of Custom CNC Components CNC-machined custom components are used across many industries. Common applications include: Automotive components Aerospace parts Robotics components Industrial machinery Automation equipment Medical equipment Tooling and fixtures Mold components Replacement machinery parts Product development Because CNC machining can accommodate different materials, geometries, and production quantities, it is suitable for both specialized components and repeat production. Why Choose Polymach365 for Custom CNC Components? Polymach365 provides digital manufacturing solutions that connect CAD designs with CNC production. Its CNC capabilities include: CNC
How Material Selection Impacts CNC Machining Cost and Performance
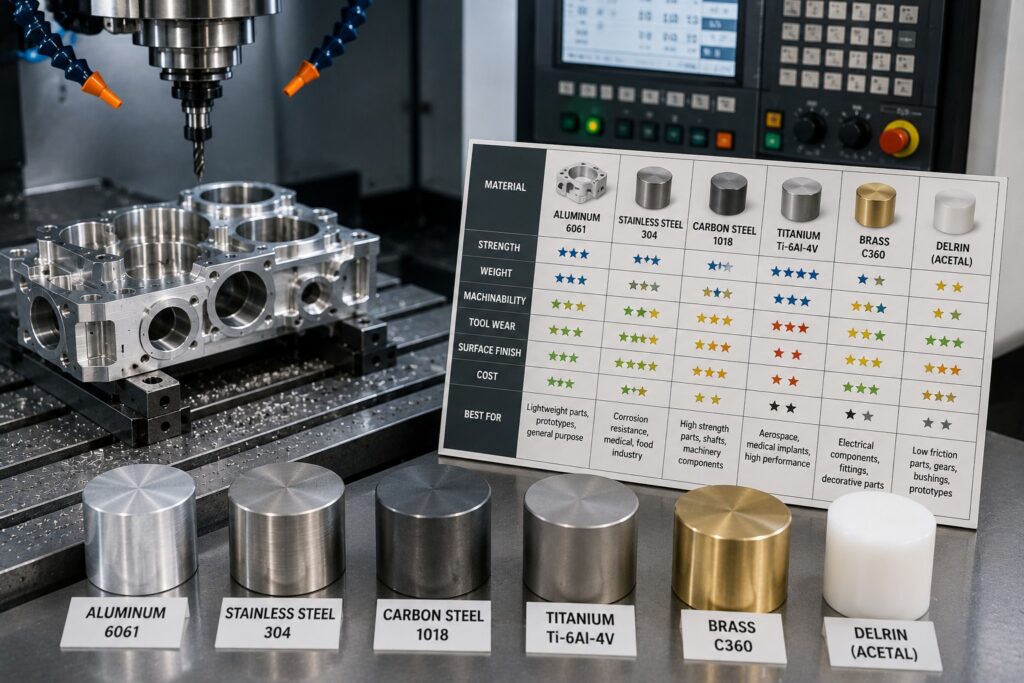
Introduction Material selection is one of the most important decisions when designing a CNC machined part. The material affects not only the strength, weight, durability, and performance of the finished component but also the machining time, tooling requirements, surface finish, and overall production cost . Therefore, choosing a material simply because it meets the basic strength requirement may not always be the best approach. Engineers and manufacturers should also consider machinability, operating conditions, dimensional requirements, finishing needs, and production volume. At Polymach365 , CNC machining supports a wide range of applications, including prototypes, custom components, low-volume production, and production parts. Selecting a suitable material at the beginning can help create a more efficient path from CAD design to finished component. Why Material Selection Matters in CNC Machining Every CNC material behaves differently during machining. For example, aluminum is generally lightweight and relatively easy to machine, while titanium offers excellent strength-to-weight performance but can require more demanding machining conditions. Similarly, engineering plastics can provide low weight and chemical resistance, but their thermal and mechanical properties differ significantly from metals. Therefore, material selection influences several aspects of manufacturing: Machining speed Cutting tool life Cycle time Surface finish Dimensional stability Part weight Strength Wear resistance Corrosion resistance Production cost As a result, selecting the right material requires balancing performance and manufacturing ability . How Material Affects CNC Machining Cost Material cost is only one part of the total machining cost. A material that costs less per kilogram may still produce a more expensive component if it requires slower machining, specialized tooling, or additional finishing. The overall cost can be influenced by: Raw material price Material availability Machining time Tool wear Cutting parameters Coolant requirements Setup requirements Surface finishing Inspection requirements Scrap and material waste Therefore, material selection should be evaluated as part of the complete manufacturing process. 1. Material Price Influences Production Cost The most obvious factor is the price of the raw material. Common CNC materials include: Aluminum Stainless steel Carbon steel Tool steel Brass Copper Titanium Alloy steel ABS Nylon Delrin Polycarbonate PEEK PTFE However, material price alone should not determine the final choice. For example, selecting a cheaper material may reduce raw material expenses but increase machining time or finishing costs. Consequently, the best material is usually the one that provides the required performance at an acceptable total manufacturing cost. 2. Machinability Affects CNC Cycle Time Machinability describes how easily a material can be cut and shaped. Materials with good machinability can often be processed efficiently with appropriate tooling and cutting parameters. Poorly machinable materials may require: Lower cutting speeds Reduced feed rates Specialized tooling Additional passes More frequent tool replacement Therefore, machinability can have a significant effect on CNC machining cycle time. 3. Material Hardness Affects Tool Wear Harder materials can place greater demands on cutting tools. For example, hardened steels may require suitable carbide tooling and carefully controlled cutting parameters. As tool wear increases, manufacturers may experience: Reduced dimensional consistency Poorer surface finish Increased tool replacement Longer production times Therefore, material hardness should be considered alongside tool selection and machining strategy. 4. Aluminum for Lightweight CNC Components Aluminum is widely used for CNC machined components because it offers a useful combination of low weight, strength, corrosion resistance, and machinability . It is commonly selected for: Housings Braces Fixtures Machine components Automotive components Prototypes Aerospace components Furthermore, aluminum can often be machined efficiently with suitable cutting tools and parameters. Therefore, it is a popular option when weight reduction and efficient machining are important. 5.Stainless Steel for Strength and Corrosion Resistance Stainless steel is frequently selected when components require strength and resistance to corrosion. Typical applications include: Industrial equipment Medical components Food-processing equipment Mechanical components Automotive parts Custom machinery However, some stainless-steel grades can be more demanding to machine than aluminum. Therefore, manufacturers may need to use appropriate tooling, cutting parameters, and coolant strategies. As a result, stainless steel can provide excellent performance while requiring more machining consideration. 6. Carbon Steel for Mechanical Applications Carbon steel can provide a useful combination of strength, durability, and cost. It is commonly considered for: Machinery components Shafts Braces Fixtures Structural components Custom mechanical parts However, the appropriate grade should be selected according to the component’s required mechanical and environmental properties. Therefore, material grade is just as important as the general material category. 7. Titanium for High-Performance Components Titanium provides an excellent strength-to-weight ratio and can perform well in demanding environments. It is often associated with applications where weight reduction and high mechanical performance are important. However, titanium can be more difficult and expensive to machine than many commonly used metals. Therefore, machining titanium may require: Appropriate cutting tools Controlled cutting parameters Effective chip management Proper coolant application Careful tool-life monitoring Consequently, titanium should be selected when its performance advantages justify the additional manufacturing requirements. 8. Brass and Copper for Specialized Components Brass offers good machinability and is commonly used for components such as: Bushings Fittings Connectors Valves Precision mechanical parts Copper, meanwhile, provides excellent electrical and thermal conductivity. Therefore, copper can be useful for: Electrical components Heat-transfer components Conductive parts Specialized industrial applications However, copper’s machining behavior differs from brass and aluminum, so tooling and cutting conditions should be selected accordingly. 9. Engineering Plastics for Lightweight Parts CNC machining is not limited to metals. Engineering plastics can be suitable for components that require: Low weight Electrical insulation Chemical resistance Low friction Dimensional stability Common options include: ABS Useful for lightweight prototypes and general-purpose components. Nylon Often selected for wear-resistant and lightweight applications. Delrin Known for good machinability, low friction, and dimensional stability. Polycarbonate Provides impact resistance and transparency in suitable applications. PEEK Used in demanding environments where high temperature and chemical resistance are important. PTFE Known for low friction and chemical resistance. Therefore, engineering plastics can provide useful alternatives to metals when the application allows. How Material Affects Surface Finish Material properties can influence the surface finish achievable through CNC machining. A material’s hardness, toughness, thermal behavior, and cutting characteristics can affect
How Surface Finish Affects the Performance of CNC Machined Parts
How Tool Wear Affects CNC Machined Part Quality Tool wear is an unavoidable part of CNC machining. As cutting tools repeatedly remove material from a workpiece, their cutting edges gradually lose their original sharpness. If this wear is not monitored and controlled, it can affect dimensional accuracy, surface finish, tolerances, production consistency, and overall part quality . Therefore, understanding how tool wear develops and how it affects machined components is important for manufacturers producing prototypes, custom parts, low-volume batches, and production components. At Polymach365 , CNC milling, CNC turning, 3-axis, 4-axis, and 5-axis machining can support a wide range of manufacturing requirements. Proper tooling and process control are essential for producing consistent CNC machined parts. What Is Tool Wear in CNC Machining? Tool wear occurs when the cutting edge of a CNC tool gradually deteriorates during machining. Every cutting operation exposes the tool to: Friction Heat Cutting forces Material contact Vibration Repeated machining cycles Over time, these conditions can change the shape and sharpness of the cutting edge. As a result, a tool that initially produces accurate components may eventually produce different results if it is not replaced or managed appropriately. Why Does Tool Wear Matter? Tool wear directly affects the relationship between the cutting tool and workpiece. A sharp tool can remove material predictably. However, a worn tool may generate more heat, cutting forces, and friction. Consequently, excessive tool wear can contribute to: Dimensional variation Poor surface finish Burr formation Chatter Increased cutting forces Longer cycle times Reduced productivity Component rejection Therefore, monitoring tool condition is an important part of CNC quality control. Types of Tool Wear Different machining conditions can produce different forms of tool wear. 1. Flank Wear Flank wear develops along the clearance face of the cutting tool. As the flank gradually wears away, the effective cutting geometry changes. Therefore, excessive flank wear can affect dimensional accuracy and surface quality. 2. Crater Wear Crater wear develops on the rake face of the cutting tool where chips flow across the cutting edge. High temperature and continuous chip contact can contribute to crater formation. As crater wear increases, the cutting geometry can change and eventually weaken the cutting edge. 3. Chipping Chipping occurs when small pieces of the cutting edge break away. It can be associated with: Excessive cutting forces Hard materials Interrupted cuts Incorrect cutting parameters Vibration Consequently, chipping can cause sudden changes in cutting performance. 4. Thermal Wear High temperatures can accelerate tool degradation. Heat can result from: High cutting speeds Excessive friction Poor coolant application Difficult-to-machine materials Improper cutting parameters Therefore, controlling heat is important for maintaining tool performance. How Tool Wear Affects Dimensional Accuracy One of the most important effects of tool wear is dimensional variation. As the cutting edge wears, it may no longer remove material in exactly the same way as a new tool. For example, a worn tool may gradually change the size of: Holes Pockets Slots Diameters Contours Mating surfaces Therefore, components produced later in a machining run may begin to move outside their specified tolerances. This is especially important when manufacturing precision components with tight dimensional requirements. Tool Wear and Surface Finish Tool condition also has a significant effect on surface finish. A sharp cutting edge generally produces a more predictable cutting action. However, a worn tool can increase friction and vibration. As a result, the machined surface may develop: Rougher texture Visible tool marks Scratches Chatter marks Irregular surfaces Therefore, surface finish should be monitored when machining components with functional or aesthetic finishing requirements. Tool Wear and Burr Formation Burrs are unwanted raised edges that can appear after machining. A worn cutting edge may produce less efficient cutting and greater deformation near the edge of a feature. Consequently, burr formation can increase. Excessive burrs may create additional requirements for: Deburring Cleaning Finishing Inspection Therefore, maintaining suitable tool condition can help reduce unnecessary secondary operations. Tool Wear Can Increase Cutting Forces As a tool becomes worn, cutting resistance can increase. Higher cutting forces can affect both the tool and the workpiece. They may contribute to: Tool deflection Workpiece movement Vibration Chatter Dimensional variation Therefore, increasing cutting forces can be an important indication that a tool requires attention. Tool Wear and CNC Machining Cycle Time Tool wear can also affect productivity. A worn tool may require: Lower cutting speeds Additional finishing passes More frequent adjustments Extra inspection Tool replacement Consequently, excessive wear can increase the effective machining time per component. For production machining, even a small increase in cycle time can become significant when multiplied across hundreds or thousands of parts. Factors That Accelerate Tool Wear Several factors influence how quickly a CNC cutting tool wears. Cutting Speed Excessive cutting speed can increase heat generation and accelerate wear. Therefore, cutting speed should match the tool and workpiece material. Feed Rate An inappropriate feed rate can increase cutting forces or reduce cutting efficiency. Depth of Cut Heavy cuts can place greater loads on the cutting edge. Workpiece Material Harder materials can cause faster tool degradation. Materials such as hardened steel and titanium may require specialized tooling and machining parameters. Coolant Proper coolant application can help manage heat and chip evacuation. However, coolant selection and application should match the machining operation. Tool Material Carbide, coated carbide, ceramic, and other tooling materials have different performance characteristics. Therefore, tool selection should match the application. How to Detect Tool Wear Manufacturers can monitor tool conditions in several ways. Visual Inspection Inspecting the cutting edge can reveal visible wear or chipping. Dimensional Inspection Measuring machined components can reveal gradual dimensional changes. Surface Finish Inspection Changes in surface quality may indicate deteriorating tool performance. Cutting Sound Changes in machining noise can sometimes indicate vibration or tool degradation. Spindle Load Changes in machine load may indicate increased cutting resistance. Tool Monitoring Systems Modern CNC equipment can use automated monitoring technologies to detect changes in machining conditions. Therefore, combining several monitoring methods can provide better control than relying on a single indicator. How to Prevent Excessive Tool Wear
How Tool Wear Affects CNC Machined Part Quality
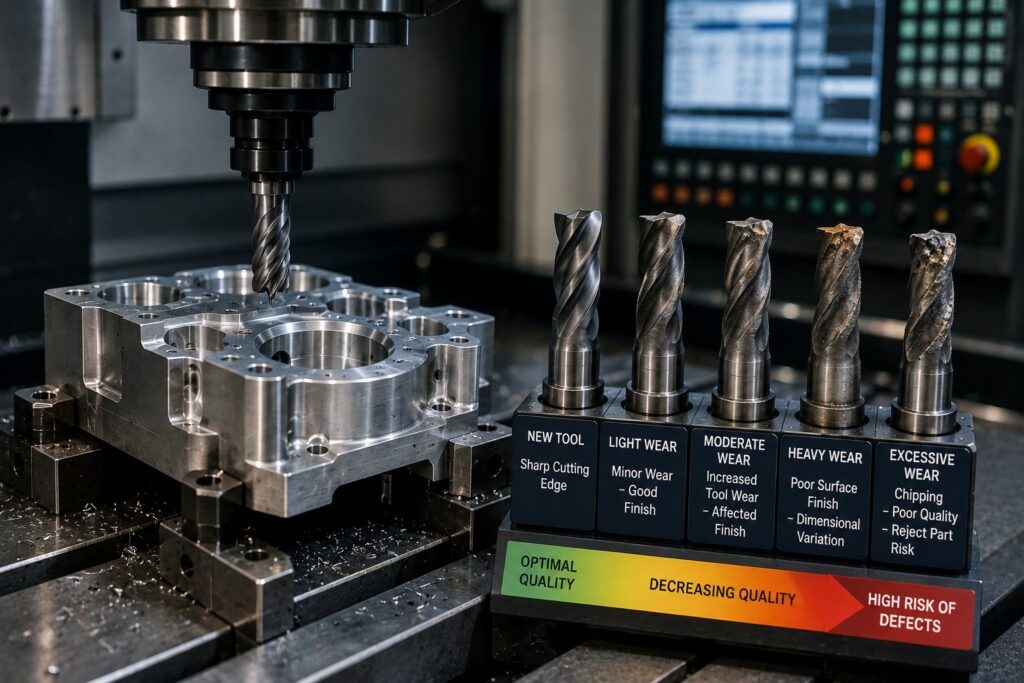
Introduction Tool wear is an unavoidable part of CNC machining. As cutting tools repeatedly remove material from a workpiece, their cutting edges gradually lose their original sharpness. If this wear is not monitored and controlled, it can affect dimensional accuracy, surface finish, tolerances, production consistency, and overall part quality . Therefore, understanding how tool wear develops and how it affects machined components is important for manufacturers producing prototypes, custom parts, low-volume batches, and production components. At Polymach365 , CNC milling, CNC turning, 3-axis, 4-axis, and 5-axis machining can support a wide range of manufacturing requirements. Proper tooling and process control are essential for producing consistent CNC machined parts. What Is Tool Wear in CNC Machining? Tool wear occurs when the cutting edge of a CNC tool gradually deteriorates during machining. Every cutting operation exposes the tool to: Friction Heat Cutting forces Material contact Vibration Repeated machining cycles Over time, these conditions can change the shape and sharpness of the cutting edge. As a result, a tool that initially produces accurate components may eventually produce different results if it is not replaced or managed appropriately. Why Does Tool Wear Matter? Tool wear directly affects the relationship between the cutting tool and workpiece. A sharp tool can remove material predictably. However, a worn tool may generate more heat, cutting forces, and friction. Consequently, excessive tool wear can contribute to: Dimensional variation Poor surface finish Burr formation Chatter Increased cutting forces Longer cycle times Reduced productivity Component rejection Therefore, monitoring tool condition is an important part of CNC quality control. Types of Tool Wear Different machining conditions can produce different forms of tool wear. 1. Flank Wear Flank wear develops along the clearance face of the cutting tool. As the flank gradually wears away, the effective cutting geometry changes. Therefore, excessive flank wear can affect dimensional accuracy and surface quality. 2. Crater Wear Crater wear develops on the rake face of the cutting tool where chips flow across the cutting edge. High temperature and continuous chip contact can contribute to crater formation. As crater wear increases, the cutting geometry can change and eventually weaken the cutting edge. 3. Chipping Chipping occurs when small pieces of the cutting edge break away. It can be associated with: Excessive cutting forces Hard materials Interrupted cuts Incorrect cutting parameters Vibration Consequently, chipping can cause sudden changes in cutting performance. 4. Thermal Wear High temperatures can accelerate tool degradation. Heat can result from: High cutting speeds Excessive friction Poor coolant application Difficult-to-machine materials Improper cutting parameters Therefore, controlling heat is important for maintaining tool performance. How Tool Wear Affects Dimensional Accuracy One of the most important effects of tool wear is dimensional variation. As the cutting edge wears, it may no longer remove material in exactly the same way as a new tool. For example, a worn tool may gradually change the size of: Holes Pockets Slots Diameters Contours Mating surfaces Therefore, components produced later in a machining run may begin to move outside their specified tolerances. This is especially important when manufacturing precision components with tight dimensional requirements. Tool Wear and Surface Finish Tool condition also has a significant effect on surface finish. A sharp cutting edge generally produces a more predictable cutting action. However, a worn tool can increase friction and vibration. As a result, the machined surface may develop: Rougher texture Visible tool marks Scratches Chatter marks Irregular surfaces Therefore, surface finish should be monitored when machining components with functional or aesthetic finishing requirements. Tool Wear and Burr Formation Burrs are unwanted raised edges that can appear after machining. A worn cutting edge may produce less efficient cutting and greater deformation near the edge of a feature. Consequently, burr formation can increase. Excessive burrs may create additional requirements for: Deburring Cleaning Finishing Inspection Therefore, maintaining suitable tool condition can help reduce unnecessary secondary operations. Tool Wear Can Increase Cutting Forces As a tool becomes worn, cutting resistance can increase. Higher cutting forces can affect both the tool and the workpiece. They may contribute to: Tool deflection Workpiece movement Vibration Chatter Dimensional variation Therefore, increasing cutting forces can be an important indication that a tool requires attention. Tool Wear and CNC Machining Cycle Time Tool wear can also affect productivity. A worn tool may require: Lower cutting speeds Additional finishing passes More frequent adjustments Extra inspection Tool replacement Consequently, excessive wear can increase the effective machining time per component. For production machining, even a small increase in cycle time can become significant when multiplied across hundreds or thousands of parts. Factors That Accelerate Tool Wear Several factors influence how quickly a CNC cutting tool wears. Cutting Speed Excessive cutting speed can increase heat generation and accelerate wear. Therefore, cutting speed should match the tool and workpiece material. Feed Rate An inappropriate feed rate can increase cutting forces or reduce cutting efficiency. Depth of Cut Heavy cuts can place greater loads on the cutting edge. Workpiece Material Harder materials can cause faster tool degradation. Materials such as hardened steel and titanium may require specialized tooling and machining parameters. Coolant Proper coolant application can help manage heat and chip evacuation. However, coolant selection and application should match the machining operation. Tool Material Carbide, coated carbide, ceramic, and other tooling materials have different performance characteristics. Therefore, tool selection should match the application. How to Detect Tool Wear Manufacturers can monitor tool conditions in several ways. Visual Inspection Inspecting the cutting edge can reveal visible wear or chipping. Dimensional Inspection Measuring machined components can reveal gradual dimensional changes. Surface Finish Inspection Changes in surface quality may indicate deteriorating tool performance. Cutting Sound Changes in machining noise can sometimes indicate vibration or tool degradation. Spindle Load Changes in machine load may indicate increased cutting resistance. Tool Monitoring Systems Modern CNC equipment can use automated monitoring technologies to detect changes in machining conditions. Therefore, combining several monitoring methods can provide better control than relying on a single indicator. How to Prevent Excessive Tool Wear Tool wear cannot be eliminated completely. However,
Why CAD Design Matters in CNC Manufacturing
Introduction Computer-Aided Design (CAD) plays a critical role in modern CNC manufacturing. Before a CNC machine begins cutting material, manufacturers need accurate digital information that defines the part’s geometry, dimensions, tolerances, holes, features, and other manufacturing requirements . A well-prepared CAD design helps manufacturers understand exactly what needs to be produced. Furthermore, it can reduce design errors, improve machining accuracy, simplify production planning, and support better quality control. At Polymach365 , digital manufacturing connects CAD designs with CNC machining processes, including CNC milling, CNC turning, 3-axis, 4-axis, and 5-axis machining, prototype manufacturing, low-volume production, and custom machined parts. What Is CAD in CNC Manufacturing? CAD stands for Computer-Aided Design . It is used to create detailed digital models of components before they are manufactured. A CAD model can define important information such as: Part dimensions Geometry Holes and slots Curves and contours Wall thickness Internal features Mounting locations Critical surfaces Design intent Therefore, CAD provides the digital foundation for CNC manufacturing. Instead of relying only on sketches or manually interpreted drawings, manufacturers can use the digital model to prepare the machining process. How CAD Connects With CNC Machining The CNC manufacturing process typically begins with a digital design. A simplified workflow is: CAD Design → DFM Review → CAM Programming → CNC Machining → Inspection → Finished Part First, the engineer creates the component in CAD software. Next, the design can be reviewed for manufacturing ability. Then, CAM software can use the design information to create machining toolpaths. These toolpaths guide the CNC machine during cutting. As a result, accurate CAD data helps create a more reliable connection between design intent and physical production . 1. CAD Improves Machining Accuracy Accurate machining starts with accurate design information. A detailed CAD model defines the intended geometry of the component. Therefore, machinists and manufacturing engineers can work from a consistent digital reference. CAD helps to communicate: Overall dimensions Feature locations Hole positions Contours Depths Angles Critical surfaces Consequently, a properly prepared CAD model can reduce misunderstandings during manufacturing. 2. CAD Helps Identify Design Problems Early Finding a manufacturing problem after production can begin resulting in wasted material, time, and money. Therefore, reviewing the CAD model before machining is important. Manufacturers can evaluate potential issues such as: Extremely thin walls Deep cavities Difficult tool access Small internal radii Unnecessary features Complex geometries Tight tolerances As a result, engineers can make improvements before the part reaches the CNC machine. 3. CAD Supports Design for Manufactureability CAD and Design for Manufacture (DFM) work closely together. A component may function correctly in theory but still be difficult or expensive to machine. For example, a design may contain a deep narrow pocket that requires a long cutting tool. Therefore, the engineer may modify the geometry to improve tool accessibility. Similarly, unnecessarily tight tolerances can increase machining and inspection requirements. Consequently, CAD provides an excellent environment for identifying and improving these issues before production. 4. CAD Makes Complex Parts Easier to Manufacture Modern CNC machines can manufacture highly complex components. However, complex geometry requires accurate digital information. CAD models can represent: 3D contours Angled surfaces Curved profiles Deep pockets Multi-sided features Complex cavities Organic shapes Therefore, CAD is particularly important when manufacturing components that require 4-axis or 5-axis CNC machining . With an accurate model, manufacturers can develop suitable machining strategies for complex surfaces and features. 5. CAD Helps With CNC Milling CNC milling is commonly used for components containing: Pockets Slots Holes Flat surfaces Contours Mounting features Complex profiles A CAD model provides the geometry needed to create the appropriate milling toolpaths. Therefore, the quality of the CAD model can directly affect machining preparation. For example, missing or incorrect dimensions may result in additional clarification or design revisions before manufacturing can begin. 6. CAD Helps With CNC Turning CAD is equally valuable for CNC turning. Turning is commonly used to manufacture: Shafts Pins Bushings Sleeves Spacers Rollers Threaded components The CAD model can define diameters, lengths, grooves, threads, shoulders, and other rotational features. Consequently, accurate CAD information helps manufacturers prepare the turning process according to the required component geometry. 7. CAD Helps Control Tolerances Not every dimension requires the same level of precision. A CAD design can identify important dimensions and tolerances that affect component performance. Critical features may include: Bearing fits Mating surfaces Hole locations Shaft diameters Sealing surfaces Alignment features Therefore, engineers should specify tight tolerances only where they are functionally necessary. This approach can help balance performance, manufacturing ability, and cost . 8. CAD Supports Prototype Manufacturing Prototype development often involves several design changes. A typical process is: Initial CAD → Prototype → Testing → Design Changes → Revised CAD → New Prototype Therefore, CAD makes it easier to modify the design and manufacture updated versions. CNC machining can then produce functional prototypes from metals and engineering plastics. As a result, engineers can evaluate fit, assembly, dimensions, and functionality before moving into production. 9. CAD Reduces Manufacturing Errors Clear digital design information can reduce communication problems between engineers and manufacturers. A good CAD package can provide a consistent reference for: Geometry Dimensions Features Manufacturing requirements Design revisions Therefore, version control is also important. Manufacturers should work from the approved and current CAD version to avoid producing outdated designs. 10. CAD Supports Faster Production Planning Manufacturers need to understand the component before deciding how to machine it. The CAD model helps them evaluate: Machine requirements Tool accessibility Workholding Number of setups Machining orientation Cutting strategy Material removal Consequently, a well-prepared CAD model can simplify production planning. This is particularly valuable for custom parts and complex CNC components. CAD File Formats for CNC Machining Different manufacturing platforms and CNC workflows may support different CAD formats. Common formats include: STEP STP IGES IGS STL SLDPRT Among these, STEP files are widely used for exchanging 3D CAD data between different software systems. However, the preferred format depends on the manufacturing workflow and required information. Therefore, it is important to provide the correct file format when requesting a
CNC Machining for Small Businesses A Practical Manufacturing Guide
Introduction CNC machining gives small businesses access to accurate, repeatable manufacturing without requiring large production volumes. From custom components and prototypes to replacement parts and small-batch production , CNC machining can help businesses turn digital designs into functional physical parts. For a small business, however, choosing the right machining process, material, quantity, tolerances, and supplier is important for controlling costs and avoiding unnecessary production delays. This guide explains how CNC machining works for small businesses, when it makes sense, what factors affect cost, and how to prepare a project for successful manufacturing. What is CNC Machining? CNC machining is a computer-controlled manufacturing process that removes material from a solid workpiece to create a finished component. A CNC machine follows programmed instructions generated from a digital CAD design. Depending on the machine and part geometry, operations such as milling, turning, drilling, boring, threading, and contouring can be performed. Common CNC machining processes include: CNC milling CNC turning CNC lathe machining 3-axis machining 4-axis machining 5-axis machining This flexibility makes CNC machining suitable for businesses manufacturing everything from simple brackets to complex mechanical components. Why Is CNC Machining Useful for Small Businesses? Large manufacturers often have dedicated production lines and high-volume orders. Small businesses may have very different requirements. They may need: A few prototype parts Small production batches Custom machine components Replacement parts Engineering samples Specialized fixtures Custom tooling CNC machining can accommodate these requirements without requiring permanent tooling dedicated to a single plastic part design. As a result, small businesses can use CNC machining to manufacture parts according to their current production needs. CNC Machining for Prototypes Product development is one of the most useful applications of CNC machining for small businesses. Instead of moving directly from CAD design to large-scale production, a business can manufacture a prototype first. A typical workflow is: CAD Design → CNC Prototype → Testing → Design Changes → Final Design → Production A machined prototype can help evaluate: Physical dimensions Assembly Fit Function Strength Usability Design problems Therefore, CNC machining can help small businesses validate products before shipping to larger quantities. CNC Machining for Small-Batch Production Not every business needs thousands of parts. Small-batch CNC machining can be useful for: New products Specialized equipment Industrial components Custom products Pilot production Replacement parts Limited-market products For businesses with unpredictable demand, producing smaller quantities can also reduce the risk of holding excessive inventory. CNC Milling or CNC Turning: Which Does Your Business Need? The right CNC process depends largely on the geometry of the component. CNC Milling CNC milling is generally suitable for components containing: Pockets Slots Flat surfaces Holes Complex contours Multi-sided features Typical examples include brackets, housings, mounting plates, fixtures, and custom machine components. CNC Turning CNC turning is generally suitable for rotational components such as: Shafts Pins Bushings Spacers Sleeves Rollers Cylindrical components If your part combines cylindrical and non-cylindrical features, it may require both turning and milling operations. Choosing the Right Material Material selection is another important consideration for small businesses. Common CNC machining materials include: Aluminum Stainless steel Carbon steel Brass Copper Titanium ABS Nylon Delrin Polycarbonate PEEK Aluminum A popular option for lightweight components and prototypes because of its useful strength-to-weight ratio and machinability. Stainless Steel Suitable for applications requiring strength and corrosion resistance. Brass Often used for fittings, bushings, connectors, and other components where machinability is important. Engineering Plastics Materials such as Nylon, Delrin, and PEEK can be useful when a component requires lower weight, electrical insulation, chemical resistance, or other specific properties. The best material depends on the part’s operating environment, strength requirements, temperature exposure, and intended application. What Affects CNC Machining Cost for Small Businesses? CNC machining costs vary from project to project. Several factors can influence the final price. Material The cost and machinability of the selected material affect the overall manufacturing cost. Part Complexity A simple component may require only a few machining operations, while a complex component can require multiple tools and setups. Machining Time Longer cutting times generally increase production costs. Number of Setups Components requiring multiple orientations may require additional setup work. Tolerances Very tight tolerances can require additional process control and inspection. Surface Finish Additional finishing requirements can increase production time and cost. Quantity The number of parts can significantly affect the economics of the project. Therefore, small businesses should consider the complete manufacturing requirement rather than focusing only on the initial machining price. How Small Businesses Can Reduce CNC Machining Costs Avoid Unnecessary Tight Tolerances Only specify tight tolerances where they are necessary for the function or assembly of the component. Simplify the Design Removing unnecessary features can reduce machining operations. Choose Practical Materials A readily machinable material may reduce manufacturing time compared with a more difficult material when both meet the application’s requirements. Reduce Setups Designing parts with machining accessibility in mind can help reduce the number of setups. Order the Appropriate Quantity Ordering too few parts can increase the per-part cost because setup costs are distributed across fewer components. Use DFM Principles Design for Manufacturing, or DFM, helps engineers create parts that are easier and more economical to manufacture. As a result, a manufacturing-friendly design can often provide better cost control. Why CAD Files Matter A clear CAD file gives the manufacturer the information needed to understand the component geometry. Common file formats may include: STEP STP IGES IGS STL DXF For CNC machining, 3D solid models such as STEP files are often useful for understanding complex component geometry. A technical drawing can also communicate important requirements such as: Critical dimensions Tolerances Threads Surface finish Material Special notes Therefore, providing complete design information can make quoting and manufacturing more simple. What Should a Small Business Provide When Requesting a CNC Quote? To receive a useful manufacturing quotation, provide as much relevant information as possible. 1. CAD File Provide the latest approved design. 2. Material Specify the required material and grade where applicable. 3. Quantity State how many components you need. 4. Tolerances Identify critical tolerances rather than
How DFM Improves CNC Machined Part Quality and Reduces Production Costs
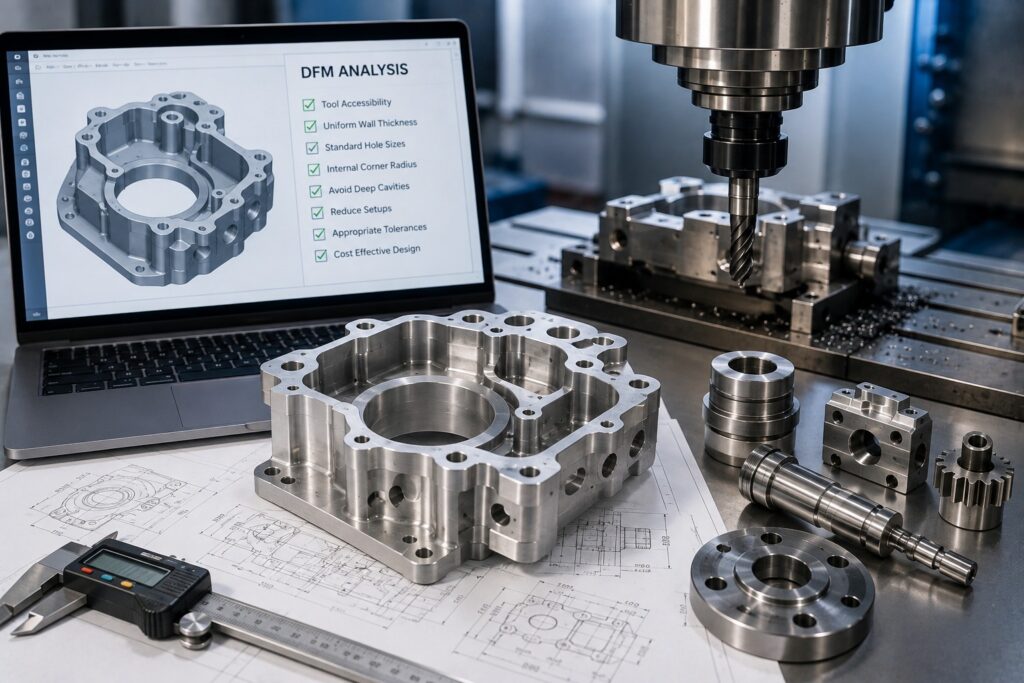
Introduction Design for Manufacturability (DFM) is an important part of CNC machining because the way a component is designed directly affects how easily, accurately, and efficiently it can be manufactured. Part may look perfect in CAD software, but that doesn’t always mean it is practical to machine. Difficult-to-access features, unnecessarily tight tolerances, deep cavities, thin walls, and complicated setups can increase machining time and production costs. Therefore, applying DFM principles before manufacturing begins can help engineers create parts that are easier to machine, more consistent, and more cost-effective . At Polymach365 , we support CNC milling, CNC turning, 3-axis, 4-axis, and 5-axis machining, prototype manufacturing, low-volume production, custom CNC machining, and precision machined components. A DFM-focused approach can help connect your design requirements with a practical manufacturing process. What Is Design for Manufacture? Design for Manufacture means designing a component with the manufacturing process in mind. For CNC machining, DFM considers factors such as: Part geometry Material selection Tolerances Wall thickness Internal corners Hole sizes Tool accessibility Machining orientation Number of setups Surface finish Production quantity Instead of designing a component first and worrying about manufacturing later, DFM encourages engineers to consider manufacturing ability from the beginning. As a result, potential manufacturing problems can be identified before production starts. Why Is DFM Important for CNC Machining? CNC machines can manufacture highly complex components. However, complexity often comes with additional manufacturing requirements. For example, a deep and narrow cavity may require a long cutting tool. However, long tools can be more susceptible to vibration and deflection. Similarly, extremely tight tolerances may require additional finishing operations and inspection. Therefore, a DFM review can identify these challenges early and help engineers make practical design decisions. 1.DFM Improves CNC Machined Part Quality One of the biggest benefits of DFM is improved manufacturing consistency. A manufacturing design allows cutting tools to reach the required features more effectively. It can also reduce unnecessary setups and minimize difficult machining operations. Consequently, manufacturers can achieve more predictable results. DFM can help improve: Dimensional accuracy Repeatability Surface finish Feature consistency Assembly fit Overall part quality Therefore, DFM is not only about reducing cost. It also contributes directly to the quality of the finished component. 2. DFM Reduces Unnecessary Tight Tolerances Tolerances define how much a dimension can vary from its nominal value. While tight tolerances are essential for certain functional features, applying them to every dimension can make a component unnecessarily expensive to manufacture. Tighter tolerances may require: Additional machining operations More precise tooling Additional inspection Longer cycle times Specialized processes Therefore, engineers should identify which dimensions are genuinely critical. Better Approach Instead of specifying extremely tight tolerances throughout the entire component, use tighter tolerances only where they affect: Mating components Bearing fits Sealing surfaces Critical alignment Functional movement As a result, the part can maintain its required performance without unnecessary manufacturing complexity. 3. DFM Simplifies Part Geometry Complex geometry can increase machining time and programming requirements. Some complex features may also require specialized tooling or multi-axis machining. Therefore, simplifying the geometry where possible can improve manufacturing ability. For example, unnecessary pockets, grooves, or decorative features may increase machining time without providing a functional benefit. A DFM review asks an important question: Does every feature serve a purpose? If the answer is no, removing that feature may reduce both machining time and cost. 4. DFM Improves Tool Accessibility Cutting tools need sufficient access to the features they are machining. Deep cavities, narrow slots, and obstructed surfaces can make tool access difficult. Therefore, designers should consider tool accessibility while developing the CAD model. Poor tool access can result in: Longer machining times Specialized tooling Additional setups Tool deflection Reduced surface quality As a result, designing features with practical tool access can make CNC machining more efficient. 5. DFM Helps Control Internal Corner Radii CNC milling tools are generally round. Therefore, creating perfectly sharp internal corners is difficult with conventional milling. Instead, internal corners normally require a radius. Why Does This Matter? If a design includes a very small internal corner radius, the manufacturer may need a smaller cutting tool. However, smaller tools can require slower cutting conditions and may increase machining time. Therefore, using the largest practical internal radius can often improve machining efficiency. 6. DFM Reduces the Number of CNC Setups Every additional setup can add time and increase positioning requirements. A component that requires machining from several directions may need multiple repositioning operations. Therefore, designers should consider whether the part can be manufactured with fewer setups. Multi-axis machining can sometimes provide better access to multiple surfaces. However, not every component needs 5-axis machining. Consequently, the goal should be to choose a design and machining strategy that provides the required features with an efficient number of setups. 7. DFM Helps Prevent Thin-Wall Problems Thin walls can be difficult to machine because cutting forces may cause vibration or deformation. Therefore, unnecessarily thin sections should be avoided when the application allows. A stronger and more stable design can help improve: Machining stability Dimensional consistency Surface finish Part rigidity However, the appropriate wall thickness depends on the material, geometry, part size, and machining strategy. Therefore, wall thickness should be evaluated together with the complete component design. 8. DFM Reduces Machining Time Machining time is an important factor in CNC production costs. Several design decisions can increase machining time, including: Excessive material removal Deep pockets Very small features Complex toolpaths Tight tolerances Multiple setups Therefore, simplifying the design can reduce unnecessary machining operations. For example, reducing a deep pocket or eliminating a non-functional feature may significantly simplify the machining process. As a result, DFM can help shorten cycle times and improve production efficiency. 9. DFM Helps Reduce Tool Wear Tool wear can affect both quality and production costs. Difficult-to-machine designs may require aggressive toolpaths, long cutting tools, or small-diameter tools. These conditions can increase tool wear. Therefore, designing parts with practical feature sizes and accessible geometry can help manufacturers use tooling more efficiently. This can contribute to: Longer tool life More consistent